


.svg)
.svg)
.svg)

How Electrification Changes Tyre Requirements for Heavy Equipment
Electrification is changing heavy equipment across ports, terminals, construction sites and mining operations. Electric reach stackers, forklifts and mining trucks are moving from pilot projects into real working environments. For operators, the focus often starts with charging capacity, battery life and energy costs. But the powertrain is only part of the equation.
The tyres still carry every tonne of machine weight and payload, transfer driving and braking forces to the ground, manage heat and maintain stability throughout the operating cycle. When the drivetrain changes, several of the conditions that determine tyre performance can change with it.
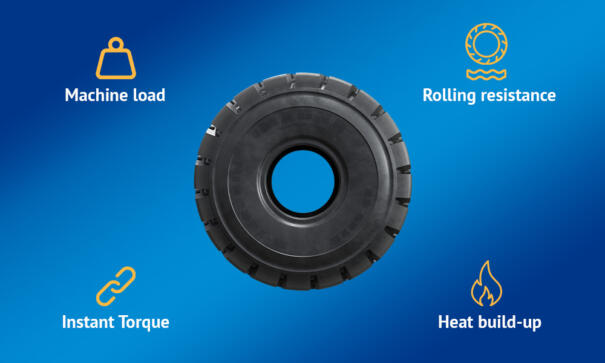
That does not mean every electric machine needs a completely different type of tyre. There is no universal “electric heavy equipment tyre”. The correct specification still depends on the application. Electrification simply adds new factors to an already demanding selection process, including machine weight, torque delivery, rolling resistance, heat build-up and duty cycle.
Why electrification changes the demands placed on tyres.
Heavy equipment tyres operate under highly demanding conditions. A reach stacker repeatedly lifts and moves containers weighing tens of tonnes. A forklift performs constant short movements and tight turns. A mining truck carries heavy payloads over uneven haul roads. In each case, tyre performance directly affects operational continuity.
Electrification can influence several variables within those applications. Battery systems can affect overall machine weight and weight distribution. Electric motors can deliver high torque from low speeds. Energy efficiency becomes more visible because avoidable losses can affect battery use and operating time.
Machine weight and load distribution remain fundamental.
Load is one of the first factors to assess when selecting tyres for heavy equipment. Electrification can make this calculation more important because battery packs and redesigned chassis layouts may change total machine mass or the way weight is distributed across the axles.
This does not mean an electric machine is automatically heavier than its diesel equivalent. Machine architecture varies between manufacturers and applications. What matters is the actual operating weight, including attachments and payload, and the load carried by each tyre during the duty cycle.
Excessive loading increases tyre deflection and can contribute to heat build-up, casing stress and premature wear. Correct inflation pressure is therefore critical for pneumatic tyres, while load capacity and structural stability remain essential across industrial and OTR applications.
A practical example comes from Reliance Transport in New Zealand. Its SANY SRSC45E electric reach stacker weighs 74 tonnes, has a maximum loading capacity of 45 tonnes and regularly completes full eight-hour shifts. During peak periods, the machine performs around 100 container movements per day. The case does not provide comparative tyre-wear data, but it demonstrates the scale and intensity at which electric container-handling equipment is already operating.
Instant torque increases the importance of traction and tread durability.
Electric drivetrains can deliver high torque from very low speeds. In heavy equipment, that torque must ultimately pass through the tyre contact patch before it reaches the ground.
The effect on tyre wear is not identical in every operation. Power-management systems, driver behaviour, surface conditions, machine load and wheel slip all influence how the tyre responds. It would therefore be too simplistic to state that electric machines automatically wear tyres faster.
However, the change in torque characteristics makes traction and tread durability important selection criteria. Applications with frequent acceleration, tight turning or loose and abrasive surfaces can place substantial forces on tread blocks and the tyre-ground interface.
This is already being considered within electric mining. Industry examples involving electric mining trucks identify high torque, rapid acceleration and heavy operating weight as important factors in tyre development. The emphasis is on grip, stability, wear resistance, bead strength and control of energy losses. For fleet operators, this reinforces the need to assess how drivetrain characteristics interact with the real duty cycle.
Why tyre rolling resistance matters for electric heavy equipment.
Rolling resistance is the energy a tyre consumes as it deforms while moving under load. Some deformation is unavoidable: the tyre must create a contact patch, absorb surface irregularities and generate traction. But that deformation also creates energy loss.
For electric heavy equipment, tyre rolling resistance becomes part of a wider energy-efficiency discussion. Energy lost through rolling resistance is energy that the drivetrain has already taken from the battery. In applications where machines need to complete intensive cycles between charging opportunities, efficiency therefore deserves closer attention.
That does not mean the lowest possible rolling resistance should become the only objective. Heavy equipment tyres must balance traction, load capacity, stability, cut resistance, wear resistance and heat resistance. Reducing rolling resistance at the expense of durability or traction can create a larger operational cost elsewhere.
Tyre condition matters as well. Incorrect pressure, excessive deflection, unsuitable loading or abnormal wear can increase resistance and negatively affect performance. This makes tyre maintenance part of the efficiency equation as fleets become more focused on energy use and operating time.
Heat build-up remains a critical performance factor.
Heat is a major factor in OTR tyre performance. As a tyre flexes under load, internal energy is converted into heat. Speed, payload, distance, inflation pressure, ambient temperature and surface conditions all influence how much heat the tyre generates.
Electrification does not automatically create more tyre heat. However, changes in machine weight, torque delivery or operating patterns can alter the thermal demands placed on the tyre. Operators therefore need to assess the complete duty cycle rather than assume that a tyre suitable for one machine configuration will perform identically on another.
In mining and earthmoving applications, TKPH remains an important tool for evaluating the relationship between tyre load and speed. A machine operating within its load capacity can still create excessive thermal stress if average speed, haul distance or operating intensity exceeds what the tyre is designed to manage.
Controlling heat supports casing reliability and tyre life, helping reduce unplanned tyre removals and protect cost-per-hour.
Duty cycle matters more than the power source alone.
A machine being electric tells you surprisingly little about the tyre it needs. A reach stacker working on a paved terminal has a different duty cycle from a mining truck operating on a rough haul road. Even two identical electric machines can place different demands on tyres if their payloads, travel distances, surfaces or operating hours differ. Before selecting a tyre, operators should understand the actual machine weight, maximum payload, axle loads, operating speed, travel distance, surface conditions, turning frequency, gradients, ambient temperature and operating hours. These conditions determine which tyre characteristics deserve the greatest priority.
Tyre requirements differ by electric heavy equipment application:
Electric reach stackers
Reach stackers combine extreme loads with repeated manoeuvring. Tyres can experience high forces during lifting, steering and directional changes, particularly where operations involve short travel distances and a high number of container movements. Load capacity, casing stability, controlled deflection, tread durability and resistance to heat build-up remain central to reliable performance.
Electric forklifts
Forklift applications typically involve frequent acceleration, braking, steering and load changes. Those repetitive movements can create concentrated wear, especially during long shifts or on abrasive surfaces. Stability, traction, load capacity and resistance to damage remain decisive, while consistent tyre performance helps protect operational continuity.
Electric mining and earthmoving equipment
Mining shows clearly why electric power does not make tyre engineering less important. Electric mining trucks still operate with heavy and variable payloads, large tyre loads, rough haul roads and demanding traction requirements.
Research into distributed-drive electric mining trucks highlights the challenge of balancing vehicle stability, tyre adhesion utilisation and energy efficiency under changing payload and surface conditions. For OTR operations, load capacity, traction, tread durability, casing reliability, heat resistance and suitability for the operating TKPH remain fundamental.
-
IND-4

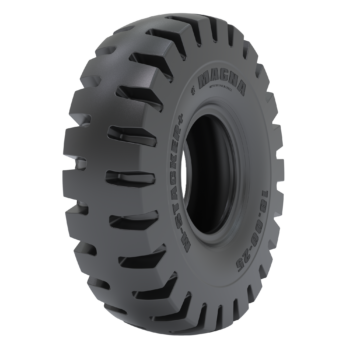
M-STACKER+
- 18.00-25
-
Solid
MA608 FORKLIFT
- 15x4½-8
- 4.00-8
- 4.80-8
- 5.00-8
- 16x6-8
- 18x7-8
- 140/55-9
- 6.00-9
- 21x8-9
- 6.50-10
- 7.50-10
- 180/60-10
- 17¾x6½-10
- 200/50-10
- 23x9-10
- 7.00-12
- 24x7-12
- 23x10-12
- 27x10-12
- 5.50-15
- 6.00-15
- 7.00-15
- 7.50-15
- 8.25-15
- 28x9-15
- 250-15 (7.00)
- 250-15(7.50)
- 300-15
- 22¼x7½-15
- 28x12.5-15
- 32x12.1-15
- 400/60-15
- 7.50-16
- 8.25-20
- 9.00-20
-
E4/L4
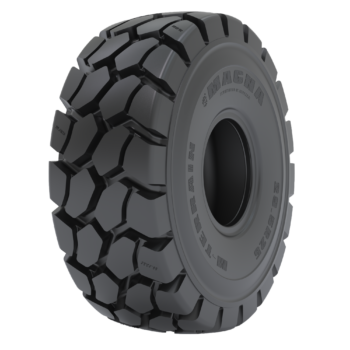
M-TERRAIN
- 20.5R25
- 23.5R25
- 26.5R25
- 29.5R25
- 750/65R25
- 875/65R29
- 33.25R29

There is no universal tyre for electric heavy equipment.
Electrification should be treated as an additional selection factor, not as a replacement for application-based tyre selection. The right tyre for an electric forklift is not the right tyre for an electric reach stacker or mining truck. Even within one machine category, differences in load, speed, surface and operating intensity can require a different specification.
This is why tyre selection should begin with operational data. Fleet managers need to understand what the machine actually does throughout a working day. Only then can tyre properties such as load capacity, traction, compound selection, tread design, casing construction and heat resistance be matched to the application.
This approach also supports a stronger Total Cost of Ownership. The lowest purchase price does not automatically deliver the lowest operational cost. A tyre that supports longer service life, predictable performance and fewer unplanned removals can create more value over its complete lifecycle.
